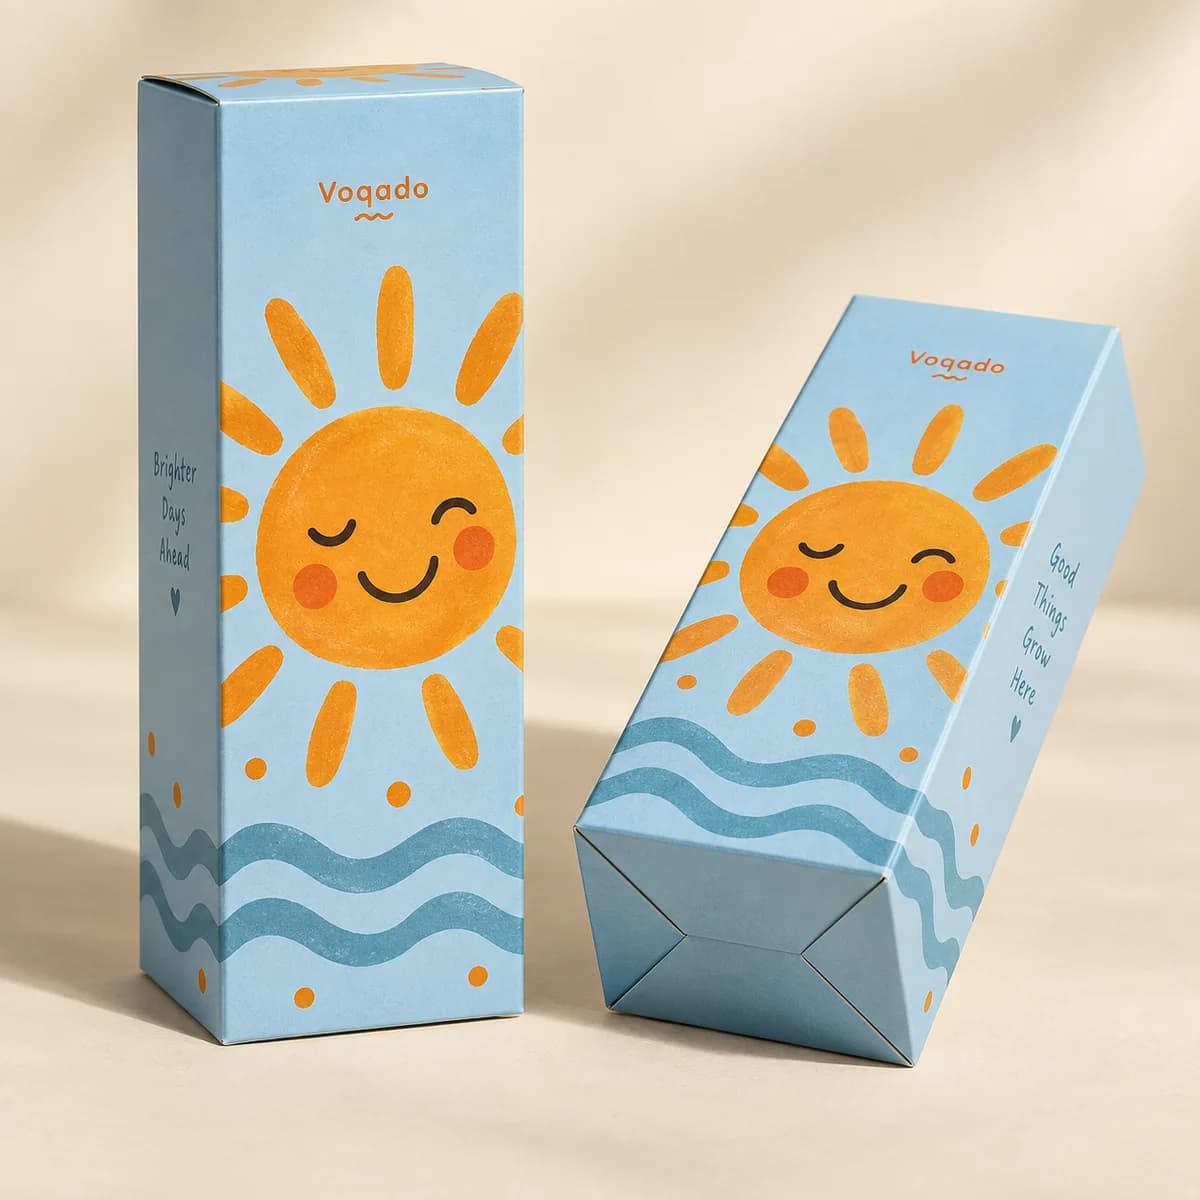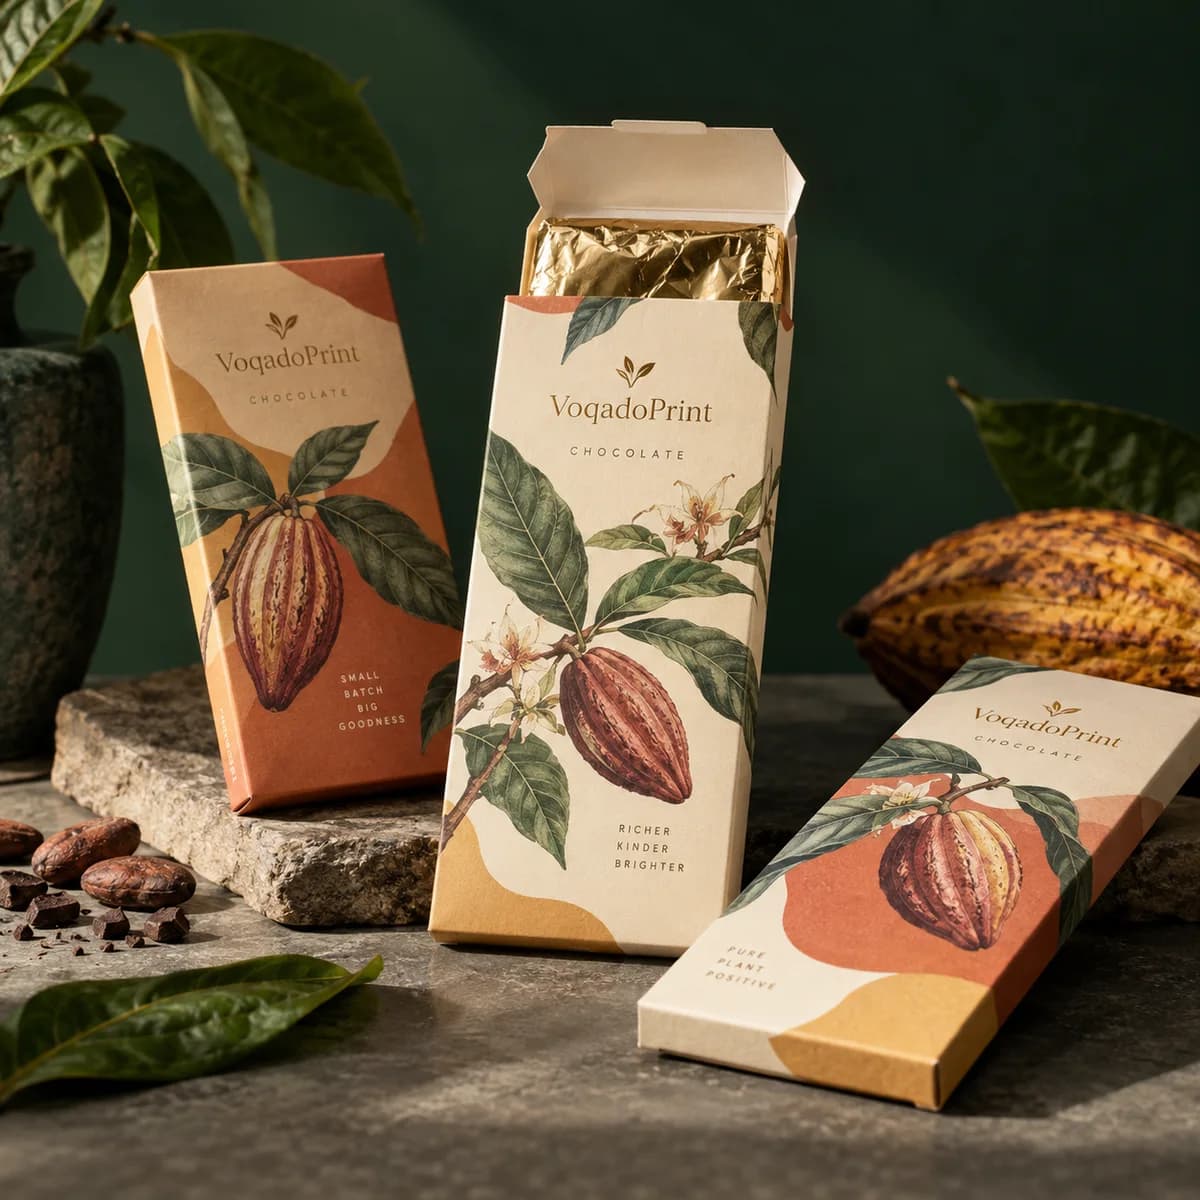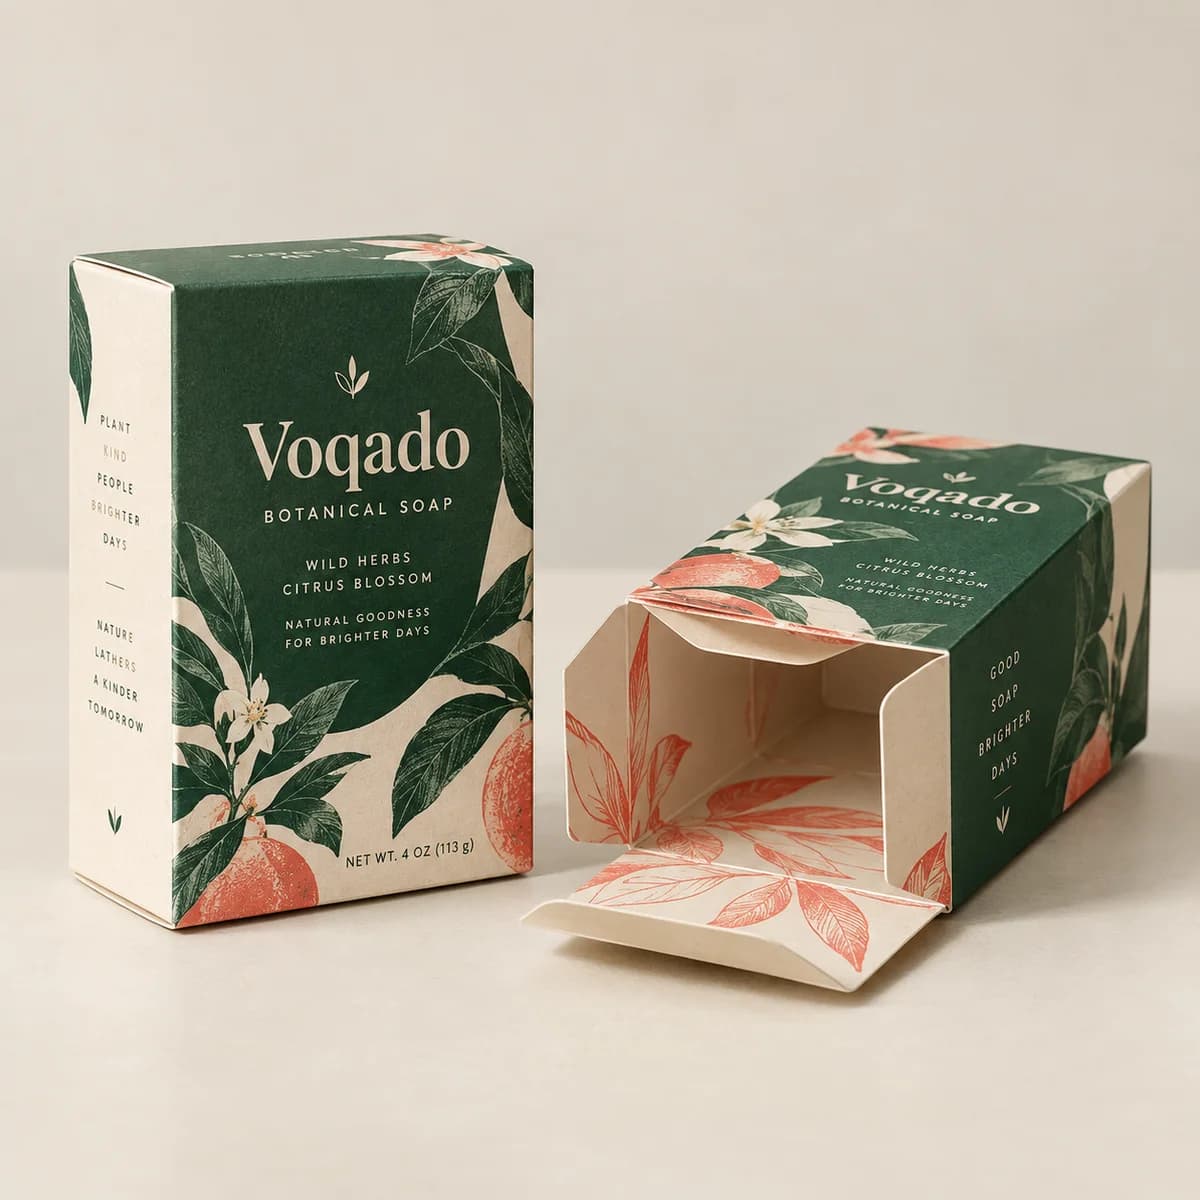
The panels, in the order they appear on the blank
Read a tuck box blank left to right and you will usually find the glue tab, then a side panel, the back, the other side, and the front. That order varies by style, which is exactly why you work on the supplied dieline rather than from memory.
| Panel | Also called | Typical content |
|---|---|---|
| Front | Face, principal display panel | Brand, product name, one selling line |
| Back | Rear panel | Ingredients, directions, barcode, contact |
| Left and right sides | End panels | Variant, net contents, short claims |
| Top tuck | Lid flap | Logo or a short line seen when opening |
| Bottom tuck | Base flap | Batch code, best before, nothing decorative |
| Dust flaps | Minor flaps | Never printed with anything that must be read |
| Glue tab | Gluing lap | Left clear of ink unless confirmed |
Width, depth and height map onto those panels in a fixed way. The front and back are width by height. The sides are depth by height. The tucks are width by roughly the depth. A tall thin box has narrow sides, which is why so much side panel copy ends up unreadable.
The glue tab is not a design surface
The glue tab is the narrow strip that bonds one end panel to the opposite edge, turning a flat blank into a tube. It is usually between 0.5 and 0.75 in wide and it is almost always folded to the inside, so nothing printed on it is visible on the finished box.
More importantly, ink, varnish and lamination sit between the adhesive and the fiber, and they can weaken the bond. Closure and sealing performance is the subject of its own standard practice, and the practical rule that comes out of it is simple: give the adhesive a clean, unfinished surface to grip. Leave the glue tab clear unless the printer tells you otherwise, and keep any full bleed background from running into it.
The same logic applies to the bottom of a glued base. If you have specified a lock bottom or auto lock bottom construction, the interlocking flaps need to move freely against each other. A thick varnish there can make a box that will not pop open cleanly on the packing table.
Which faces end up inside
On a tuck box the inside of every panel is the reverse of the printed face, so if you want an inside print you are paying for a second side. On a mailer box with a front tuck closure, the inside of the lid is the first thing the customer sees, which is why inside print is worth more there than on a retail carton that is opened once and thrown away.
The dust flaps fold in first and are partly covered by the tuck, so anything printed on them is glimpsed rather than read. Treat them as texture, never as a place for a message.
The bottom tuck faces down on a shelf. Use it for the practical marks that have to exist somewhere: batch number, lot code, date. A design that puts the logo there is paying for print nobody sees.
Orientation traps to check before approval
Panels on a flat blank are not all the same way up once folded. The classic error is a back panel that reads upside down because the blank was laid out for a reverse tuck, where the top flap folds from the back and the bottom flap folds from the front.
- Rotate a copy of the artwork on screen the way each panel folds and read every line.
- Check that a design crossing from front to side continues at the right height on both.
- Confirm the barcode sits flat on a single panel and never crosses a crease.
- Look at where a full bleed photo meets a crease; creasing cracks heavy ink coverage.
- Verify that side panel type is large enough to survive a 1.5 in wide panel.
The cheapest way to catch all five is a paper mock up. Print the flat artwork at full size, cut it out, fold it and hold it. Five minutes there saves a production run.
Panels on other constructions
Not every package has six flat panels. A pillow box has two curved faces and folded end flaps, so the usable area is the flat center band and the curve pushes edge content out of view. A slide open box is two pieces, a printed sleeve and an inner tray, and the tray is a separate blank with its own panels. A gable box adds a peaked top and a punched handle, which removes usable area from exactly where a logo wants to go.
Each of those has its own dieline, and the panel names change with it. Ask for the drawing for the specific style and size, and read its legend rather than assuming the six panel model applies.
Panel planning checklist
- Get the dieline and identify every panel by name before you design.
- Put the brand and one selling line on the front, and the required detail on the back.
- Keep the glue tab and glued bottom flaps clear of ink and coating.
- Use the bottom tuck for codes and dates rather than decoration.
- Decide whether inside print earns its cost for this specific package.
- Rotate each panel on screen and read it as it will be seen.
- Fold a full size paper mock up before approving artwork.
Frequently asked questions
What are the panels on a box called?
Front, back, left side, right side, top tuck and bottom tuck, plus small dust flaps on the side panels and a narrow glue tab at one end of the blank. The front and back are width by height, and the sides are depth by height.
Should I print on the glue tab?
No, unless the printer specifically confirms it. The tab is folded inside so nothing on it is visible, and ink, varnish or lamination sitting between the adhesive and the board can weaken the bond that holds the box together.
Which panel is the front of a box?
The panel a customer sees first on a shelf, often called the principal display panel. On the flat blank it may not be the leftmost panel, which is why you identify it from the dieline legend rather than from the drawing order.
Why did my back panel print upside down?
Most likely the style is a reverse tuck, where the top flap folds from the back and the bottom flap folds from the front, so the two panels are laid out in opposite orientations on the blank. Rotating each panel on screen or folding a paper mock up catches it.
Sources & specification notes
The references below support the relevant technical or product details in this guide. Examples and checklists are not claims of practical testing or universal supplier requirements. Confirm the current specifications for your chosen product before production.
- ASTM D1974/D1974M: Methods of Closing, Sealing, and Reinforcing Fiberboard Boxes ↗
Standard practice covering closing and sealing methods, cited for the principle that the bonded surface determines closure performance.
- FEFCO: the code developed by FEFCO and adopted by ICCA ↗
The international code system that names box constructions, so a style can be specified precisely rather than described.